ENDE
Featured Presta-compatible valve cores, high-flow tubeless stems, and ultra-lightweight TPU inner tube assemblies.
A comprehensive analysis of material selection, seal micro-geometry, and integration trends for modern cycling OEM and aftermarket distributors.
As the global cycling market pivots aggressively toward high-pressure road setups, tubeless gravel configurations, and ultra-lightweight Thermoplastic Polyurethane (TPU) inner tubes, the humble Presta valve core has transitioned from a commodity component into a critical high-precision pressure management mechanism. Modern pneumatic systems demand zero-air-loss retention under dynamic flexural loading, extreme chemical resilience against liquid latex sealants, and microscopic dimensional tolerances.
For international buyers, sourcing directly from a qualified China wholesale Presta cores manufacturer offers undeniable economies of scale. However, navigating the vendor landscape requires strict technical evaluation of alloy purity, elastomeric O-ring compounds, stem thread pitch uniformity (UNJ / French metric standard compliance), and automated quality validation. Premium Presta Valve Cores (Removable Valve Cores - RVC) engineered in top-tier Chinese facilities utilize multi-spindle Swiss-type CNC lathes, achieving tight concentricity that prevents valve stem distortion during pump head engage/disengage cycles.
The structural integrity of a Presta core relies on the alloy choice for its central pin, threaded housing, and lower seal holder. Our manufacturing processes enforce strict raw material testing via optical emission spectrometers to prevent stress corrosion cracking (SCC) under high pressure.
| Specification Parameter | Standard Commercial Brass (C36000) | Lead-Free Premium Brass (C3604 / Eco-Brass) | Aircraft-Grade Anodized Alloy 7075-T6 |
|---|---|---|---|
| Tensile Strength (MPa) | 340 - 400 MPa | 420 - 480 MPa | 540 - 580 MPa |
| Corrosion Resistance | Standard Nickel Plating (3-5μm) | Electroless Nickel Plating (8-12μm) | Hard Anodized Oxide Film (15-20μm) |
| Unit Mass (per 1,000 pcs) | approx. 1,450 grams | approx. 1,420 grams | approx. 480 grams (∼67% Weight Saving) |
| Sealant Chemical Stability | Moderate (Susceptible to Ammonia) | High (Ammonia & Glycol Resistant) | Ultra-High (Inert to Liquid Sealants) |
| Target Application | Standard Butyl Tubes / Mass Market | OEM High-End Tubes & Tubeless Stems | Ultralight TPU Tubes & Professional Racing |
Air leakage in Presta systems rarely stems from metal structural failure; over 94% of pneumatic drops occur at the lower sealing cup interface. Standard OEM suppliers frequently utilize cheap NBR (Nitrile) rubber seals that harden, shrink, or crack when exposed to cold temperatures or synthetic tire sealants. Advanced manufacturing in China now integrates dual-seal architectures:
Why tier-1 global bicycle brands, inner tube factories, and tubeless valve distributors choose our manufacturing facilities in China.
Utilizing high-speed Japanese Tsugami multi-axis CNC machines to achieve micro-tolerances of ±0.005mm on valve threads, ensuring flawless mating with rim stems, extensions, and pump heads.
Every single Presta valve core undergoes automated dual-stage pressure drop testing at 15 Bar (220 PSI) differential pressure before automated sorting and packaging, guaranteeing zero-defect shipments.
Emulating world-class quality systems (such as Austrian Tubolito standards), every bulk master carton and inner box carries laser-etched batch identifiers to track raw material heat numbers and machine shift logs.
Proprietary surface passivation and co-molding technical expertise for seamless sonic-welding or adhesive integration with ultra-lightweight Thermoplastic Polyurethane bicycle inner tubes.
Complete custom branding options including laser logo engraving, high-precision custom thread colors (Orange, Stealth Black, Red, Electric Blue, Gold), and tailored retail packaging.
Scalable production lines capable of outputting 500,000+ units per day with flexible MOQs, customized bulk polybagging, automated blister carding, and fast DDP air/sea freight logistics.
Strategic market analysis for procurement directors, product managers, and supply chain executives.
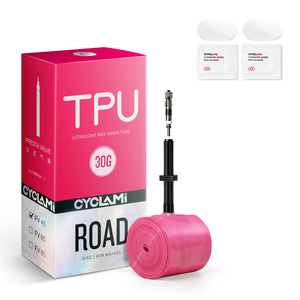
The traditional butyl inner tube, weighing between 100g to 150g per road unit, is rapidly losing market share in high-performance segments to ultralight TPU tubes weighing as little as 23g to 38g. This transition directly impacts valve core sourcing requirements. Unlike butyl rubber, which allows brass stems to be vulcanized onto thick rubber patches, TPU requires direct ultrasonic bonding or high-adhesion polymer valve stems. Manufacturers are now procuring specialized Presta cores engineered with lightweight anodized aluminum stems or composite bodies that drastically reduce rotational weight at the rim perimeter, granting cyclists immediate watt savings and responsive acceleration.
With tubeless tire adoption reaching over 70% in gravel and mountain biking disciplines, traditional Presta cores face significant operational bottlenecks. Micro-bore internal dimensions often restrict high-volume airflow required to seat tubeless bead locks, while liquid latex sealants dry within the core mechanism, causing valve freezing. Future procurement strategies emphasize High-Flow Presta Cores featuring enlarged internal fluid channels (increasing airflow by up to 300%) and anti-stick PTFE-coated brass shafts that resist chemical adhesion from ammonia-based and eco-friendly latex sealants.
Following modern consumer trends such as Tubolito’s PSENS technology, valve systems are evolving into digital diagnostic hubs. Next-generation Presta core housings are being engineered to house or interface with miniature passive NFC pressure sensors. Procurement teams must prepare for hybrid core designs that seamlessly pair mechanical air release pins with digital pressure telemetry components, providing real-time PSI data directly to rider head units without mechanical pressure gauges.
Strict European Union REACH regulations and California Proposition 65 mandates are accelerating the phase-out of traditional free-machining brass containing trace lead contents (C36000). Forward-thinking China manufacturers are shifting 100% of export production to lead-free brass alloys (such as C3604 or Eco-Brass) and recyclable 7075 aluminum alloys. B2B buyers must audit supplier material certificates to ensure compliant cross-border Customs clearance and eliminate toxic metal exposure across retail packaging.
A technical evaluation guide for auditing China Presta core manufacturers.
When evaluating potential wholesale suppliers in China, purchasing managers should perform rigorous technical verification across four core operational pillars:
| Audit Dimension | Technical Verification Standard | Red Flag / Quality Risk |
|---|---|---|
| Thread Fitting Accuracy | Pass/Fail Go-NoGo gauge checking for outer 5V2 rim threads and inner 8V1 core threads. Precision pitch within ISO 9001 specs. | Loose threads causing core blowout under high PSI (>110 PSI); stripped threads during pump attachment. |
| Plating Durability | Salt spray corrosion test exceeding 48 hours (ASTM B117 standard) for nickel plating thickness (≥8μm). | Flaking nickel coating clogging valve orifice; rapid surface oxidation in wet outdoor environments. |
| Pneumatic Seal Integrity | 100% automated pressure decay testing at 1.5× working pressure (15 Bar) with nitrogen/air bubble chamber testing. | Micro-leakage through lower rubber seal resulting in overnight tire pressure loss (>0.5 Bar/24hr). |
| Spring Tension Stability | Stainless steel 304 internal spring fatigue tested for >10,000 depression cycles with consistent spring rate recovery. | Weak internal spring causing valve pin to stick open after manual pressure adjustment or gauge check. |
Clear answers to technical, commercial, and logistical questions regarding wholesale Presta core procurement.